A publican converting a back kitchen in Dublin – or fitting out a gastropub in Cork or Galway – will meet two vendors very quickly: one selling a hood, one selling a planning headache. The difference between them shows up in four places: the airflow calculation behind the canopy, the odour treatment stage, the cleaning and documentation regime, and the way the design answers a neighbour complaint before it starts. This article works through the pub cookline load, the Irish rules that shape the specification, a sizing example near 6,600 m3/h, and a checklist built to survive a local authority query.
What an Irish pub kitchen actually puts in the air
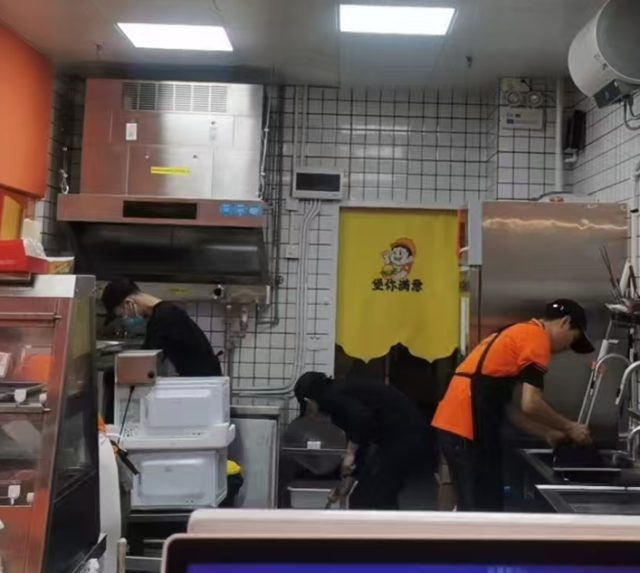
The modern Irish pub kitchen has drifted a long way from sandwiches and crisps. The typical cookline now carries a two- to three-basket fryer bank for fish and chips, chicken goujons and burger sides, a flat-top griddle running burgers and breakfast items from early morning, and a carvery or roast counter on weekend service. The fryer bank and griddle are the particulate problem: deep frying at 170-190 degrees C generates a dense grease aerosol whose sub-micron fraction passes straight through metal mesh, while the griddle adds carbonised residue and smoke spikes every time a patty hits the plate. The carvery contributes the opposite problem – almost no grease, but a heavy plume of aromatic vapours from roasting meat and gravies that is an odour issue rather than a filtration one.
This split drives the same two-phase logic that governs every serious kitchen design. The particulate phase – grease aerosol, carbonised residue, breadcrumb dust – must be separated first, because any adsorption stage placed upstream of adequate grease separation saturates within weeks. The gaseous phase – cooking odour compounds – is handled after particulate removal, by an activated carbon stage sized on residence time rather than a catalogue label. A quote that collapses both phases into one “odour filter” line item is the most common specification failure in this segment, and it is the first thing to test in any Irish pub tender.
The Irish rules that decide the specification
Ireland regulates kitchen exhaust through four instruments, and unlike some jurisdictions the wording is refreshingly direct about who carries the burden.
Section 24 of the Air Pollution Act 1987. The occupier of any premises other than a private dwelling must use the best practicable means to limit, and if possible prevent, an emission from the premises, and must not cause or permit an emission in such a quantity or manner as to be a nuisance. Critically, subsection (3) makes “best practicable means have been used” a statutory good defence in any prosecution. Under section 26, a local authority can serve a notice requiring measures where it appears necessary to prevent or limit air pollution. For a pub kitchen above or beside residences, this is the clause a frying-smell complaint activates – and the operator who can produce a documented treatment chain (separator specification, ESP Cell or equivalent, carbon stage with stated mass, commissioning measurements) has a defence; the operator who cannot, does not. Irish local authorities commonly accept the UK DEFRA guidance on the control of odour and noise from commercial kitchen exhaust systems (January 2005) as the practical benchmark for what “best practicable means” looks like in this sector.
Article 33 of the Planning and Development Regulations 2001. Where a kitchen fit-out needs planning permission or a conditions response, local authorities routinely request further information on the ventilation, filtration and odour controls – including discharge location and treatment specification. In Georgian Dublin and other protected-structure areas, a new roofline discharge can be the hardest single item to obtain, which pushes the design toward recirculating or low-discharge architectures that need less planning negotiation.
Building Regulations Part F and the workplace acts. Part F sets fresh-air supply rates for the building; for kitchen staff areas the practical guidance figures run around 15 L/s per person and higher where cooking load is significant. Separately, the Safety, Health and Welfare at Work Act 2005 obliges the employer to provide air free from fumes and cooking contaminants, and the HSA enforces it – documented ventilation failures can attract improvement notices. On the fire side, the Fire Services Acts 1981 and 2003 place a duty on the person in control of premises to take reasonable measures against fire; Irish fire-safety practice for food service leans on IS 3218 for detection and alarm, IS 291 for extinguishers (a Class F wet chemical unit is the cooking-oil item), and a fire risk assessment that explicitly covers the grease extract path.
Cleaning and access standards. Irish specifications overwhelmingly point to the BESA family: DW/172 for kitchen ventilation system design, and TR19 Grease for duct cleaning and the access provision it requires. TR19-style practice ties cleaning frequency to use: roughly annual for light use up to 6 hours a day, six-monthly for pubs and restaurants in the 6-12 hour band, and quarterly for heavy 12-16 hour operations. Insurers increasingly ask for the cleaning certificate – a pub that cannot produce one after a duct fire has a coverage problem as well as a compliance one.
A sizing worked example you can take to tender
Take a representative pub kitchen: a fryer-and-griddle line of 2.4 m of hood (two basket fryers plus a flat-top griddle), and a 1.2 m section over the carvery counter and gravy station. Using the widely applied heuristic of roughly 2,000 m3/h per metre of hood for heavy frying and griddling, and around 1,500-2,000 m3/h per metre for roast-and-serve duty:
Fry and griddle section: 2.4 m at about 2,000 m3/h/m gives 4,800 m3/h. Carvery section: 1.2 m at 1,500-2,000 m3/h/m gives 1,800-2,400 m3/h. Combined design airflow: approximately 6,600 m3/h – call it a 6,500-7,000 m3/h extraction duty. Cross-check capture: a 2.4 x 1.1 m canopy presents about 2.6 m2 of opening; at 6,600 m3/h (1.83 m3/s) the face velocity lands near 0.8-0.9 m/s once filter area is accounted for – within recommended capture practice when the canopy overhangs the appliance edge by 150-300 mm. If a vendor quotes 3,000 m3/h for this cookline, the capture arithmetic alone shows the plume will escape an open fryer during Friday fish-and-chips service.
The odour stage follows from the same numbers. At 6,600 m3/h, an activated carbon bed with a 0.2 second residence time needs about 0.37 m3 of media; at roughly 465 kg per m3, that is approximately 170 kg of carbon. A quote saying “carbon filter included” without a kilogram figure is likely offering a cassette of a few kilograms that saturates in days on a fry-heavy load. Fan duty: with roughly 500-560 Pa of system pressure across duct, baffle filters, ESP Cell and carbon bed, a 700-800 Pa class centrifugal fan is the defensible selection, and the shaft power at 1.83 m3/s and 700 Pa is about 2.1 kW – so a 3 kW motor rating is the honest specification.
Ducted, ductless, or cabinet: the Dublin building decision
Irish pub kitchens sit inside some of the least duct-friendly building stock in Europe: Georgian terraces with protected facades, lanes with apartments directly over the kitchen, and beer gardens where the neighbours are three metres from the discharge point. Three routes exist, and the building – not the vendor catalogue – should pick.
Where a genuine duct run to a ridge or high-level discharge can be built and the planning conditions allow it, a full extract line with an in-line treatment train is the conventional answer; the ducted ESP purifier range covers that high-volume end, with the ESP Cell taking the particulate phase and the carbon stage handling odour before discharge. Where the facade is protected or the discharge point would face a bedroom window, recirculation is the practical architecture: a ductless all-in-one hood that pairs washable grease separation with an ESP Cell and an activated carbon stage, returning cleaned air to the kitchen instead of the neighbour’s window. The honest caveat mirrors the Irish statute: recirculation is not an exemption from section 24 – it is a way of engineering the emission down so the “best practicable means” defence is real rather than rhetorical. The carbon mass, not the brochure, decides whether that defence holds.
Two Irish-specific variations complete the picture. First, the beer garden and festival circuit – from local food fairs to the outdoor season at coastal resorts – puts cooking where no fixed cookline exists; the mobile food cart line covers ventless street-side cooking with its own integrated treatment, which is also the clean answer to a market-stall pitch. Second, back kitchens in older terraces often have 2.3-2.5 m ceilings with joists crossing exactly where an in-line stack would go; a floor-standing cabinet unit joined to a shallow canopy by a short duct decouples purification from the hood height, and the ductless range hood family includes compact cabinet formats for exactly this retrofit case.
Ten items the quote must contain
Each item is checkable on delivery, which is what turns a quotation into a contract – and, in Ireland, into evidence.
1. Design airflow in m3/h per hood section, with the sizing basis stated. 2. Face-velocity check at the canopy aperture, computed, not asserted. 3. Grease separation stage specified by type and standard (baffle filters or ESP Cell per EN 16282-6). 4. Activated carbon mass in kilograms and claimed residence time in seconds. 5. Fan curve showing the operating point at calculated system pressure, with motor rating. 6. Access provisions: tool-free filter removal, ESP cell slide-out, carbon replacement path, and access panels on any ducted run at the intervals TR19 Grease cleaning actually requires. 7. Planning and defence file: the document set that answers an Article 33 information request and supports a section 24 best-practicable-means defence – treatment specification, commissioning measurements, discharge drawing where ducted. 8. Fire documentation: the extract path noted in the fire risk assessment, IS 3218-compliant detection where required, Class F extinguishing provision, and a fixed suppression system per EN 16282-7 / EN 17446 on ducted builds. 9. Cleaning schedule written into the offer: baffle filters hot-washed weekly in fry-heavy kitchens, ESP cell wash every 2-4 weeks by load, carbon replacement per pressure-drop or calendar, professional duct cleaning on the TR19 bands. 10. Commissioning report with airflow measured at the hood, plus a warranty split that names collector plates, sealing strips, insulators and carbon as priced consumables.
What an inspection day actually tests
It helps to reverse the viewpoint: instead of asking what to buy, ask what a visiting officer or an insurance surveyor will open first. The Environmental Health Officer, auditing under the food hygiene framework where Regulation 852/2004/EC places responsibility squarely on the operator, will look at the canopy and its filters for visible grease, at condensation on walls and ceilings, and at whether the extraction and the fresh-air supply actually work together – a kitchen with strong extraction and no make-up air runs negative, whistles at the back door, and drafts cold air across the pass, and inspectors note it. The fire risk assessment reviewer will trace the grease path from fryer to discharge: filter type, duct access panels, the date on the last professional clean, and whether the Class F extinguishing provision and detection coverage match the layout. The local authority air-pollution officer, responding to a complaint, will ask exactly one engineering question – what means have been used to limit the emission – and will judge the answer by documents, not adjectives. Every one of those files traces back to items on the checklist above. That is the practical reason the quote must specify carbon mass, access spacing and commissioning measurements: those numbers are what the operator will be reading aloud one day to somebody with a clipboard.
A one-line summary for the negotiation: “Airflow per section with sizing basis, carbon mass in kg, commissioning airflow measured at the hood, and the document file that answers a local authority query.” The vendor who answers those four in writing is almost always the one whose other six numbers hold up.
How the constraints map to equipment
Translating the checklist into hardware: the fry-and-griddle pub cookline wants a ductless all-in-one hood with a deep grease separation stage ahead of an ESP Cell, which is what the ND-series provides, with the Odor Removal Tower as the carbon stage when the kitchen sits under dwellings or beside a beer garden. For a carvery-led kitchen where the load is roast vapour rather than fryer grease, a lighter unit such as the N-series paired with the Odor Removal Tower follows the same two-phase logic at lower airflow. On conformity: units built and CE certified place on the Irish market under the EU framework, and the production behind the Souniny line at Shenzhen Shuangni Environmental Technology Co., Ltd. has carried CE certification since its early product generations – which simplifies the document set at handover and for the operator’s compliance file.
The economics close the argument. Carbon at roughly 170 kg per bed is an annual consumable at fry-heavy loads; ESP cell washing is an hour of labour every fortnight. Set against one activated section 26 notice from a local authority – or an insurer declining a duct-fire claim for want of cleaning records – the specification that survives the ten-item checklist is the cheapest line in the project budget.